Residual Stress and Deformation Analysis of Steel Sleeve Repair Welding of API 5L X65 Specification in Gas Pipeline Using Simulation Approach
DOI:
https://doi.org/10.37934/afhme.10.1.2842aAbstract
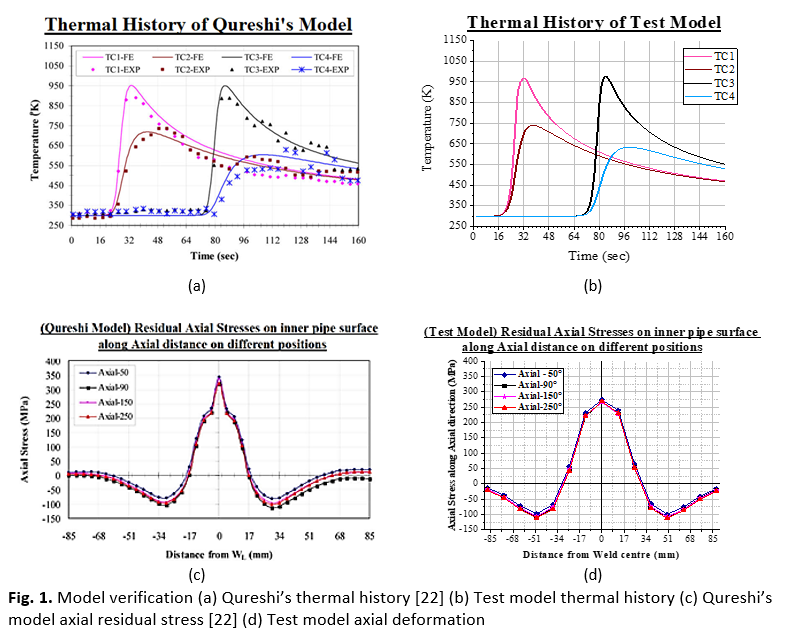
Sleeve welding repair is one of the medium scale maintenance jobs for gas pipeline. It is widely used due to avoid gas pipeline shutdown. However, there were issues raised on weldment quality and pipe burn-through. The weld quality issues were mainly resulted from excessive residual stress and deformation. The purpose of study was to determine the suitable steel sleeve dimensions and gas pipeline internal flow conditions that minimized the residual stresses and deformation. For accuracy, the pipe was modelled according to API 5L X65 standard while the steel sleeve was modelled according to properties of ASTM A131-74 grade AH. Apart from that, the weldment was modelled according to AWS standard E7018 electrode as-weld properties. The 3-dimensional model was created using SolidWorks 2018 whereas the numerical simulation was done using ANSYS v19.2. In order to achieve the objective, the study has focused on studying the thermal history, residual stresses and deformation on the pipe. From the numerical simulation, it was found that, sleeve-to-pipe gap exceeding 3 mm has increased the residual stress significantly. Then, the result has indicated there were no prominent relation between sleeve length, residual stress and deformation. From the thermal history results, there were no sign of burn-through. The increment of gas flow rate and pressure has also increased the weld cooling time while reduced the residual stress and deformation. For this study welding process, 200mm long and 8.5mm steel sleeve with no gap under 20m/s flowrate, 4.4 MPa was chosen as suitable setup.